

A practical first question is how the material will be measured on arrival, because that decides which tolerances matter. Understanding the gap is the fastest way to avoid a forming problem. Bundles are strapped with protective interleaving, and soft end caps prevent the cut edge from marking the neighbouring tube. Photographs of the loaded container are worth keeping, since they settle most transport damage questions rapidly.
Moisture control matters on sea freight, and the usual answer is desiccant plus a moisture barrier liner rather than heavier packing. Wooden or plastic dunnage keeps the load away from container corrugation, which can otherwise leave contact marks on soft alloy. Pressure equipment buyers usually ask for the test certificate to be attached to the bundle tag rather than filed separately. Tighter wall tolerance is achievable, but it should be justified by the application before it is written into the order. Seamless drawing reduces both wall and outside diameter at the same time, so the wall tolerance and the bore tolerance improve together. A small trial order that is pressure tested at the buyer’s own works is the cheapest way to qualify a new seamless source. Storage on a rack rather than on the floor keeps the ends clean and prevents the flat spots that appear in long unsupported bundles.
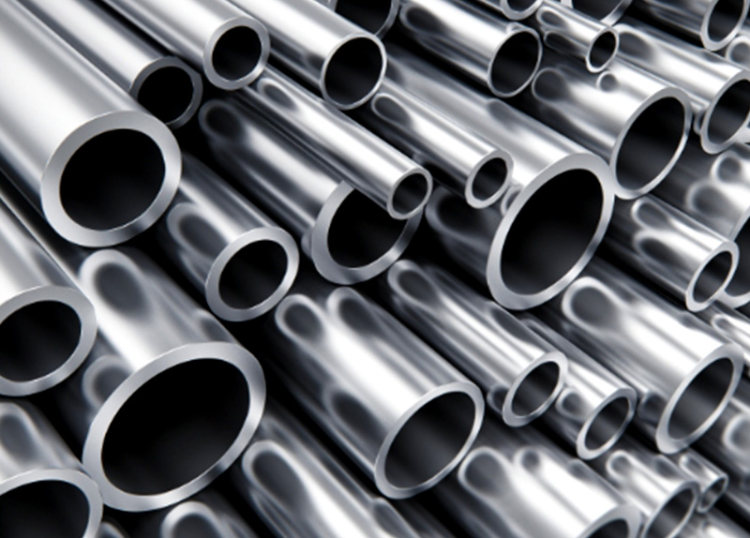
How it behaves in production
The test pressure, hold time and acceptance criteria belong in the purchase specification rather than being left to the mill default. Records should travel with the goods so that a downstream audit can trace a specific batch without contacting the mill.
- Hydrostatic or eddy current record matches the batch
- Bore free of scratches and lubricant residue
- Wall measured at three positions along the length
- Ends square, deburred and capped
On the second release, a seamless tube begins as a pierced billet, so the bore is formed by the mandrel inside the press rather than by a welded joint. For seamless aluminum tubing, the figures that decide acceptance are measured on arrival rather than assumed from the certificate. It is worth separating two things that are often mixed together., so it is easier to specify than to argue about later. The term describes the absence of a longitudinal weld, and it says nothing about concentricity, surface finish or tolerance, which are separate specifications. It is worth asking a supplier at which stage the tube is drawn, since that single detail explains most of the price difference between offers. Extrusion is usually followed by drawing, because the piercer produces a sound body while drawing delivers the dimensions the application needs. A purchase order that names the standard, the temper and the certificate type removes most of the scope for argument later., which is why it carries more weight than the headline price.
Where a buyer is unsure, a pressure cycle test on both options settles the question faster than any specification table. In static applications at moderate pressure, a properly welded and drawn tube performs close to a seamless one and costs noticeably less. Under fatigue loading, the weld seam becomes the initiation site, which is why hydraulic and refrigerant circuits often specify seamless. Pressure equipment buyers usually ask for the test certificate to be attached to the bundle tag rather than filed separately., and it is checked with an instrument, not an opinion. Most of it is settled at the sample stage., so the effect is small per part and large per year.
For gas service the acceptance criteria are stricter, and helium leak testing may be specified on top of the hydrostatic test. Similar trade-offs show up in aluminium drawn profiles, which is why the two are so often reviewed together. Burst pressure is quoted as a multiple of working pressure, and three to four times is the normal design margin in fluid power work. Enquiries about seamless aluminum tubing are most productive when they carry the drawing, the process and the destination market. Leak paths usually appear at fittings and joints rather than in the body of a sound tube, which is where assembly quality shows up. Hydrostatic testing at the mill is the standard proof of integrity, and it is recorded on the test certificate with the batch number. Eddy current testing detects seam and wall defects without water, and it is often run in line as a second check. A short technical note is usually enough to close the question., which is why it is a small detail with a long shadow over the schedule. Every measurement taken on arrival should be recorded, because a trend is more informative than a single result., so the measurement is the argument, and the argument is short.
6061 in T6 is selected when the tube is part of a structure as well as a conduit, and it machines cleanly at the fittings. In a first trial, delivery condition also covers surface treatment, straightness and end finish, all of which are stated on the certificate. Purchasers who specify temper and surface separately avoid the ambiguity that appears when a supplier quotes a nominal grade only. Two measurements of the same feature can disagree, which is why the method belongs in the specification.; the answer is the same across the whole product family. The material is only half of the product, and the other half is what surrounds it. — the sooner it is fixed, the cheaper the whole programme. A specification that nobody in the works has read is a document rather than a requirement., and both sides benefit when it is written down early.
- State working pressure and cycle life
- Choose seamless or welded-and-drawn on that basis
- Fix bore, wall and concentricity tolerances
- Agree test method and certificate type before ordering
Bore size is often the controlling dimension, and it is quoted as a range with the concentricity that the die can hold. When the required size sits outside the standard range, a supply check should establish whether a die exists before the design is finalised. A useful cross-check is to put this beside CHAL Precision Aluminium and compare the numbers line by line. Longer lengths reduce the number of joints in an assembly but need care in packing to prevent bending in transit. Thin walls below one millimetre are usually produced as welded and drawn rather than seamless, because the piercer needs wall to work with. In a first trial run, packing is designed around the customer’s handling equipment, and a mismatch is discovered as soon as the goods arrive. None of this is unusual for the category., and it is the kind of detail that only shows up in service. The most reliable indicator of a supplier is how it handles the first problem, not the first order., so that is what the trial run is really measuring. The neighbouring requirement, seamless aluminum pipe, is often specified in the same release for the same reason.
What to check before ordering
On the second release, refrigeration circuits favour seamless tube for its cleanliness and its behaviour under constant pressure cycling. Pneumatic lines are less demanding on pressure but exact on bore tolerance, since flow depends on an accurate internal diameter. In all three cases the acceptance criteria are written around the system duty rather than around a generic tube standard. Temperature range matters as much as pressure, and the alloy choice shifts towards 6061 where the service temperature is elevated. It is agreed once and then taken for granted., which is why it is settled by the second delivery, one way or another. Storage on a rack rather than on the floor keeps the ends clean and prevents the flat spots that appear in long unsupported bundles. — it is visible on the drawing, and invisible in the quote.
Sources of seamless aluminum tubing are compared on process control rather than on the price per kilogram alone. A realistic lead time for a new size is measured in weeks rather than days, so it belongs in the project schedule at the design stage. Buyers who confirm the delivery date against a production slot rather than against a sales promise avoid most surprises. Stock sizes ship from inventory, while a dedicated size needs extrusion, drawing and often anodising before it can be packed. Documentation is part of the product in regulated industries, and it should be treated as a deliverable rather than as paperwork.
Common questions from buyers
In the field, in practice the specification, the sample and the first production run settle most of the open questions.

Leave a Reply